Regular maintenance gives you a repeatable way to inspect your printer and record changes. It cannot guarantee successful prints or replace troubleshooting. Use this checklist alongside the instructions for your exact printer, build plate, and hotend.
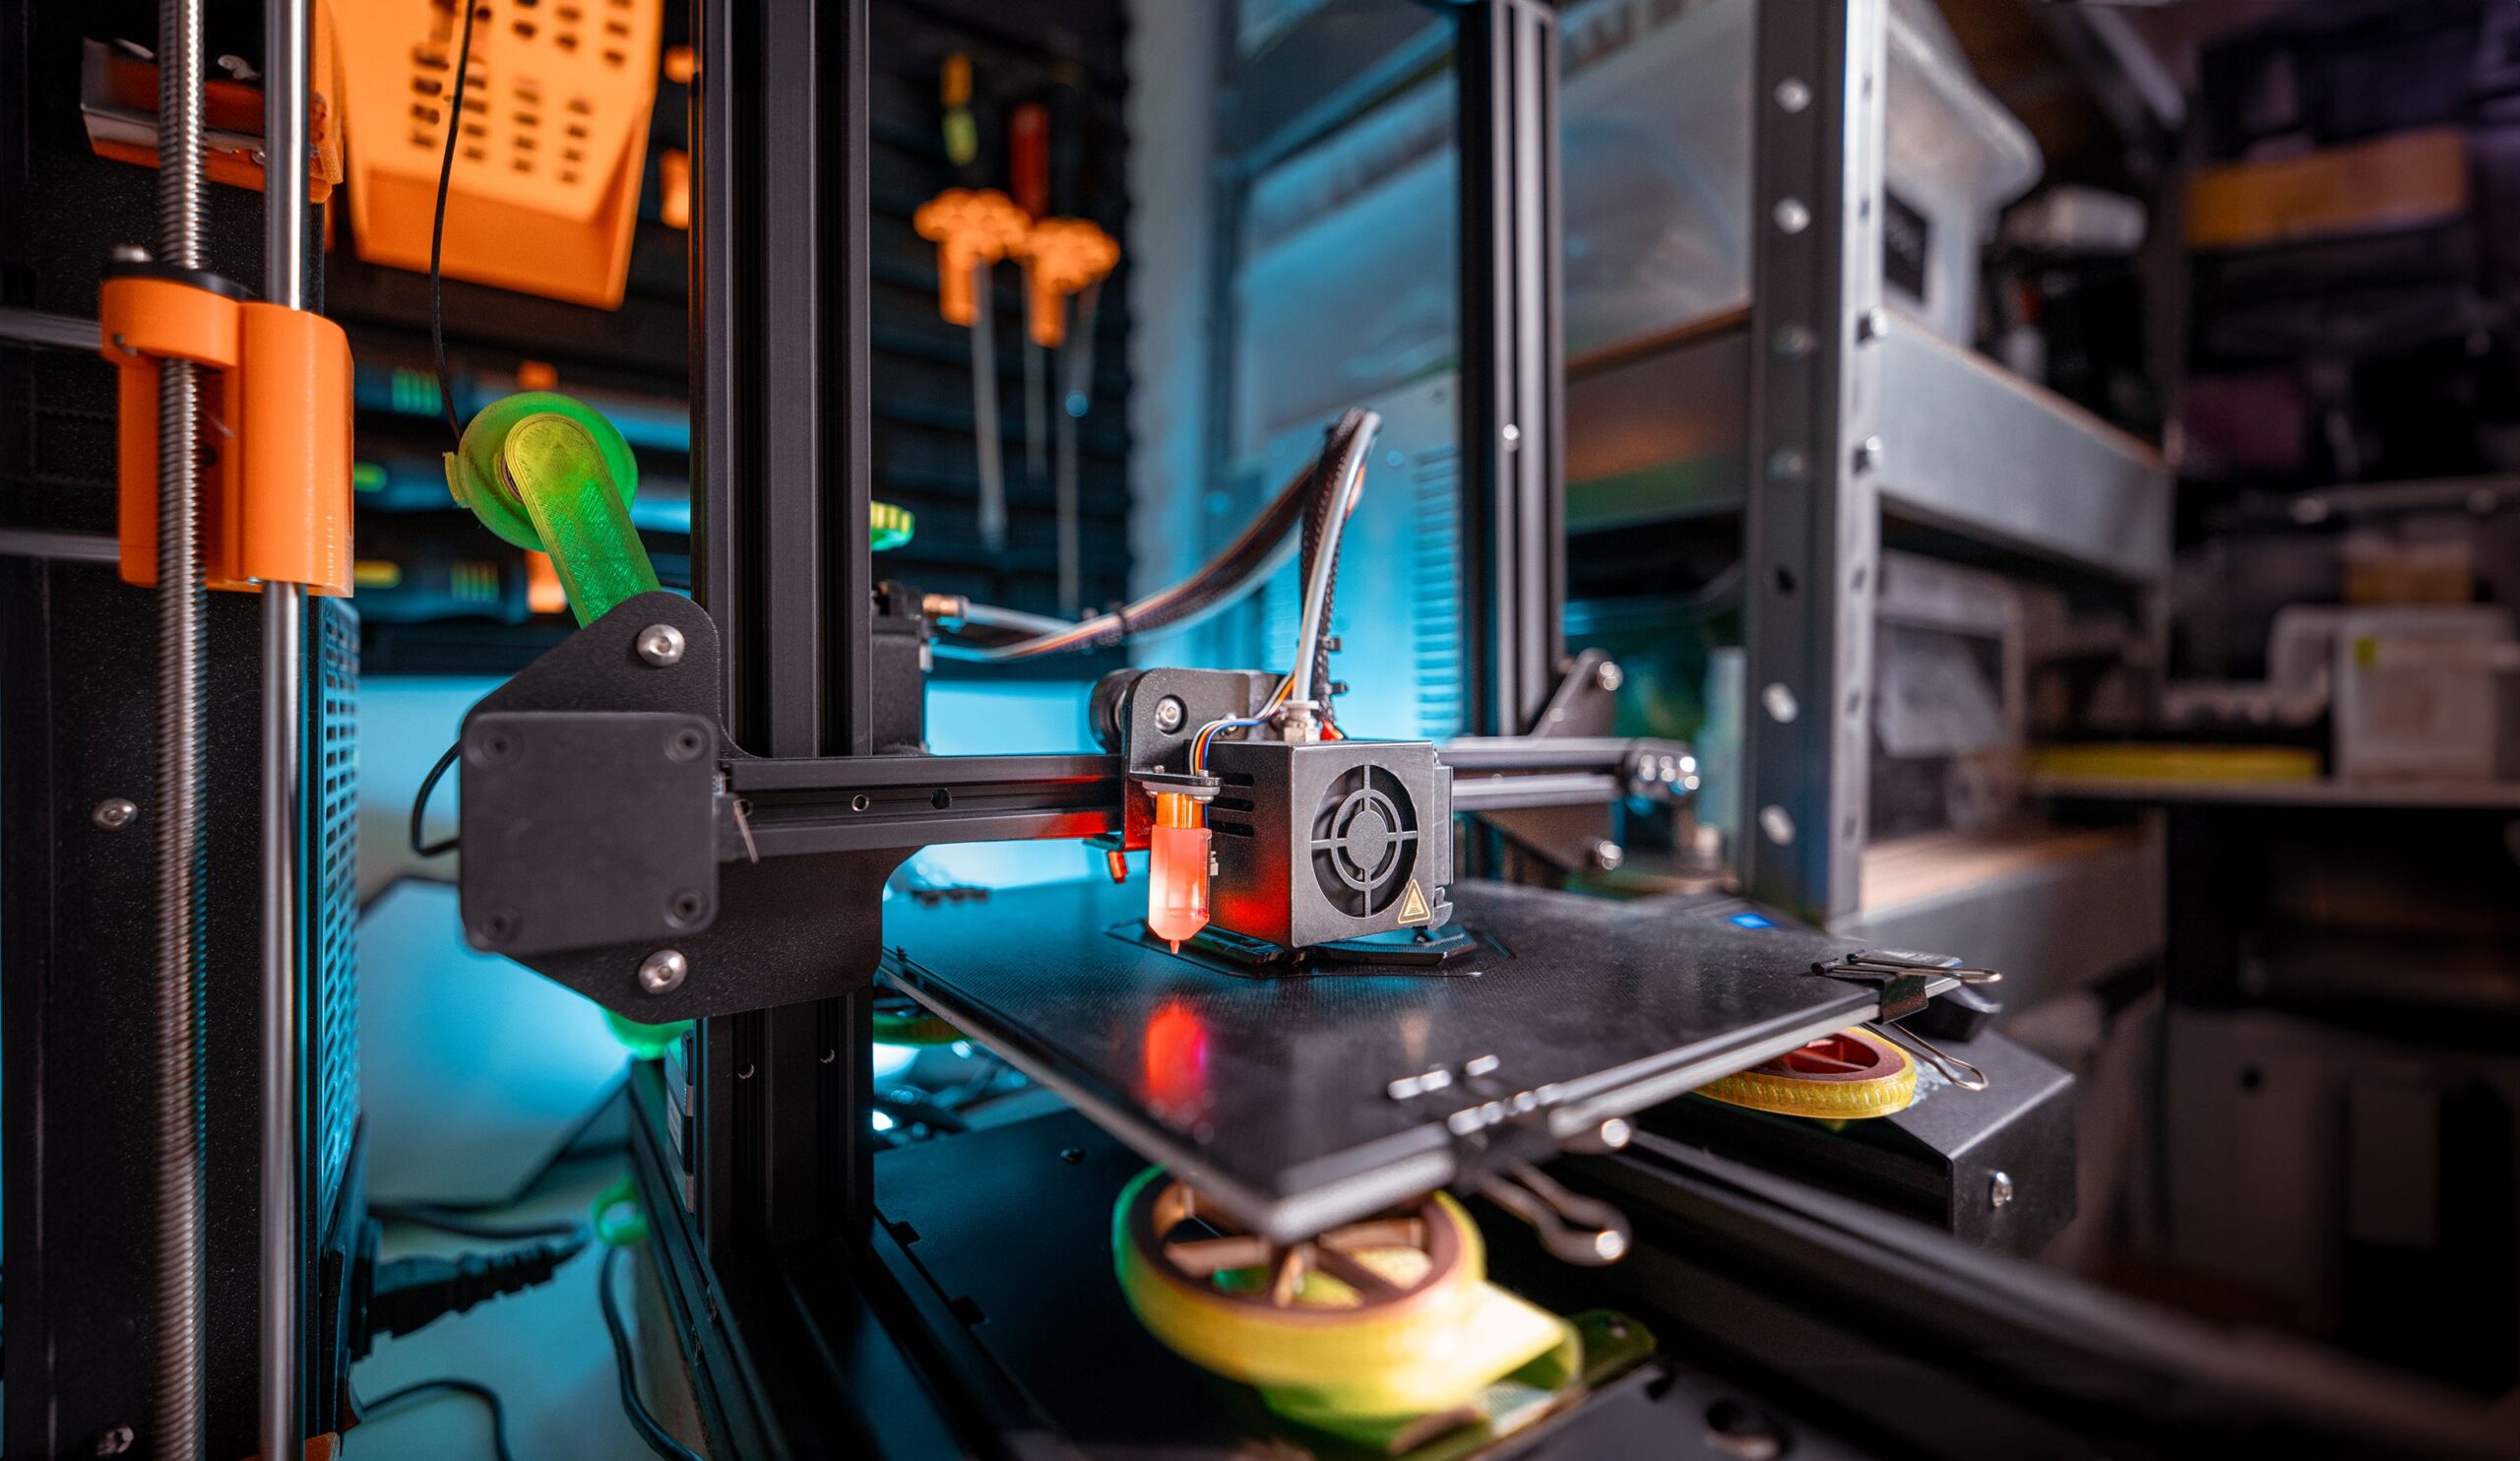
Photo by Jakub Zerdzicki on Pexels.
Before each print
- Check for loose filament scraps and debris around the printer.
- Check the build surface using its approved cleaning instructions.
- Note unusual noise, visible damage, or a new error before starting another job.
Clean the correct build surface
Cleaning products are not interchangeable. Prusa specifically prohibits IPA and other alcohol-based solvents on its PA Nylon sheet. It also prohibits acetone on its textured and satin sheets. Identify your surface before choosing a cleaner.
Lubricate only the specified parts
Check which components require lubrication and which product your manufacturer recommends. For example, Prusa specifies lubricant for the MK4/S and MK3.9/S smooth rods and bearings, but explicitly says not to lubricate their Z-axis threaded lead screws or trapezoid nuts.
Use the documented hotend-cleaning procedure
Follow the procedure for your hotend rather than using a universal temperature or tool. Prusa’s brass-brush instructions warn against touching hotend cables because the brush can cause a short circuit. Heated components also present a burn hazard.
Schedule maintenance by your printer’s requirements
A calendar reminder can help, but service intervals may depend on printing hours. Prusa lists certain MK4/S and MK3.9/S checks at 200-hour intervals; that interval should not be applied automatically to other printers.
Keep a simple maintenance record
Record the date, printing hours if available, symptoms, work performed, replacement-part numbers, and settings changed. Change one thing at a time when troubleshooting so you can judge its effect.
Use the manufacturer’s replacement, calibration, and filament-drying instructions when those tasks are needed. Keep the relevant manual links in your maintenance record so the next service starts with the correct procedure.
Check belts, pulleys, and frame hardware on a schedule
A printer is a machine that shakes itself thousands of times per print. Over weeks and months, that vibration loosens things. Two failure modes show up again and again, and both are cheap to prevent.
First, belts. The toothed belts that move the print head and bed stretch slightly with use, and a loose belt shows up as layer shifts, ghosting (faint echoes of sharp corners), or circles that print as ovals. Many printers have a tensioning mechanism — a screw, a sliding mount, or on some models an automatic tensioner. Your manual shows the correct method and how tight is tight enough; “guitar-string tight” is folk advice, not a specification, and over-tensioning wears bearings faster.
Second, frame hardware. Periodically check the bolts and screws that hold the frame, gantry, and bed together. You are not torquing them like an engine rebuild — you are checking that nothing has worked loose. A wobbly frame produces the same artifacts as a loose belt, and it is maddening to chase slicer settings for a problem that is mechanical.
How often? Tie it to the same printing-hours log the article already recommends. A quick belt-and-bolt check every few hundred hours, or whenever print quality degrades without a settings change, catches both problems early. And as with everything on this page: if your manufacturer publishes a specific check or interval, theirs wins.
Keep filament dry and stored properly
Most print quality problems people blame on the printer are actually the filament. Plastic filament absorbs moisture from the air — some types (nylon and PETG are the notorious ones, but even PLA picks it up in humid shops) — and wet filament prints with popping, hissing, stringing, and weak layer adhesion. If a roll that printed fine last month suddenly misbehaves, moisture is the first suspect, not the extruder.
Storage is the fix, and it is boring: keep rolls you are not actively using in sealed bags or bins with desiccant, not sitting open on a shelf. Desiccant packs are cheap and rechargeable in an oven or food dehydrator if yours supports it. For rolls that have already absorbed moisture, filament dryers exist — but check your filament manufacturer’s drying guidance for temperature and time rather than guessing, because too much heat deforms the roll.
One practical habit: when you open a new roll, note the date on the spool or in your maintenance record. Six months from now, when a print fails, “opened March, stored sealed with desiccant” versus “been sitting out since spring” tells you exactly where to look first.
Inspect the nozzle and replace it before it fails
Nozzles wear out. A standard brass nozzle printing plain PLA lasts a long time, but abrasive filaments — glow-in-the-dark, carbon-fiber-filled, wood-filled, metal-filled — erode the nozzle opening measurably, sometimes within a single roll. The symptom is subtle at first: extrusion gets inconsistent, fine details lose sharpness, and eventually the nozzle opening is visibly wider than spec.
Replacing a nozzle is a normal consumable swap, not a repair, but do it the way your manufacturer documents: nozzles are changed hot (with the heater at temperature) on most machines, which means burn protection and the right tools, and the heater block must be held steady so you do not snap anything. If you print abrasives regularly, consider a hardened steel or coated nozzle — but note that hardened nozzles conduct heat differently than brass, so your temperature settings may need a small adjustment. Again: the filament maker and printer maker publish the guidance; start there.
Keep one spare nozzle of the size and type your printer shipped with. When you need it at 9 PM on a Sunday, you will be glad it was a two-dollar part already in the drawer.
Update firmware through official channels only
Manufacturers release firmware updates that fix bugs, improve motion control, and occasionally add features. Checking for updates every few months is reasonable maintenance — but only install firmware from your printer manufacturer’s official site or their own update tool.
Third-party and community firmware exists and can be excellent, but it is a modification, not maintenance. It can change thermal safety behavior, and installing the wrong build for your board revision can brick the printer. If you ever go that route, treat it as a project with its own research, not as a routine update.
When you do update, record the firmware version in your maintenance log alongside the date. If a print problem appears right after an update, that version number is the first thing you will want to know — and the first thing support will ask for.
What a good maintenance log entry looks like
The article recommends keeping a record; here is what one entry actually contains. Concrete beats thorough — you will keep doing it if it takes sixty seconds:
2026-09-14 — 1,240 hrs. Noticed faint ringing on Y-axis corners. Checked belt tension per manual; tightened Y tensioner 1/4 turn. Frame bolts all snug. Swapped to fresh desiccant in dry box. Test cube printed clean. Next: nozzle has ~400 hrs on it, order a spare.
Date, hours, symptom, what you did, what you changed, and what is coming next. That is the whole system. When a problem returns six months later, this is the difference between “I think I fixed this before” and knowing exactly what worked.
Manufacturer reference
The Prusa examples above come from its official maintenance guide for MK4/S and MK3.9/S printers. These examples show why maintenance instructions need to match the machine and print surface.
The DIY Geek — hands-on guides for electronics, 3D printing, woodworking, and smart home.