Reliable crimps come from matching four things: the wire, the terminal, the applicator or hand tool, and the manufacturer’s crimp specification. A generic squeeze that looks tight is not enough.
This guide covers small low-voltage projects. It is not a procedure for household branch-circuit wiring, utility power, airbags, vehicle braking or safety systems, aircraft, medical equipment, or other regulated work.
Start with the terminal documentation
Identify the exact terminal series and download its application specification. Confirm:
- permitted conductor size and strand construction;
- insulation diameter range;
- strip length;
- approved tool, die, locator, and tool setting;
- conductor and insulation crimp dimensions;
- inspection and pull-force requirements.
AWG alone is not enough. Two wires with the same gauge can have different strand counts, insulation diameters, plating, or temperature ratings. Likewise, red, blue, and yellow insulation colors are common on some pre-insulated terminals but are not a universal sizing system.
Choose the correct tools
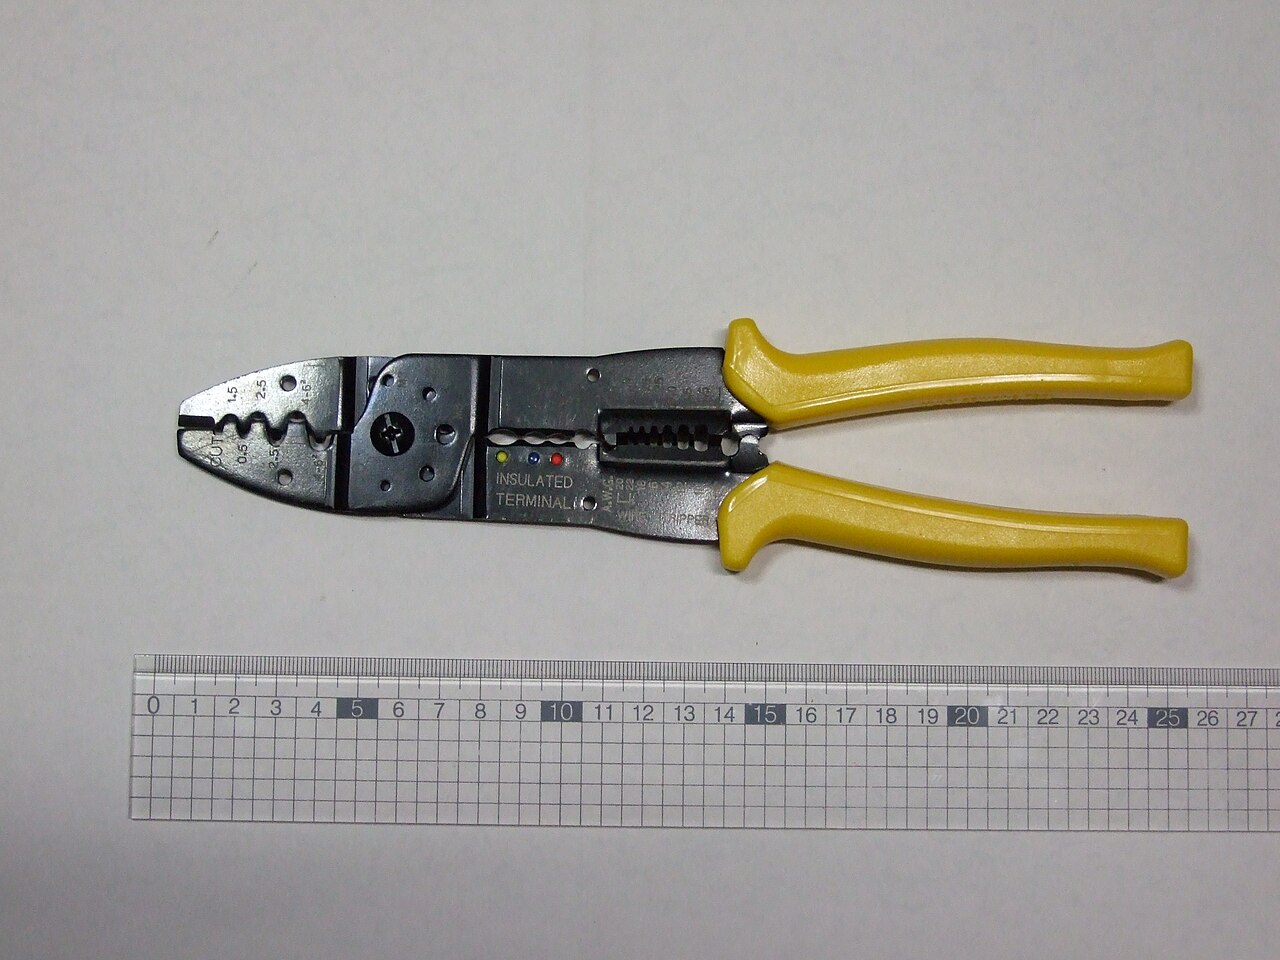
- Wire cutter: makes a square cut without crushing the conductor.
- Stripper: supports the actual conductor and insulation range. Self-adjusting models are convenient, but their range is model-specific and they still need setup and inspection.
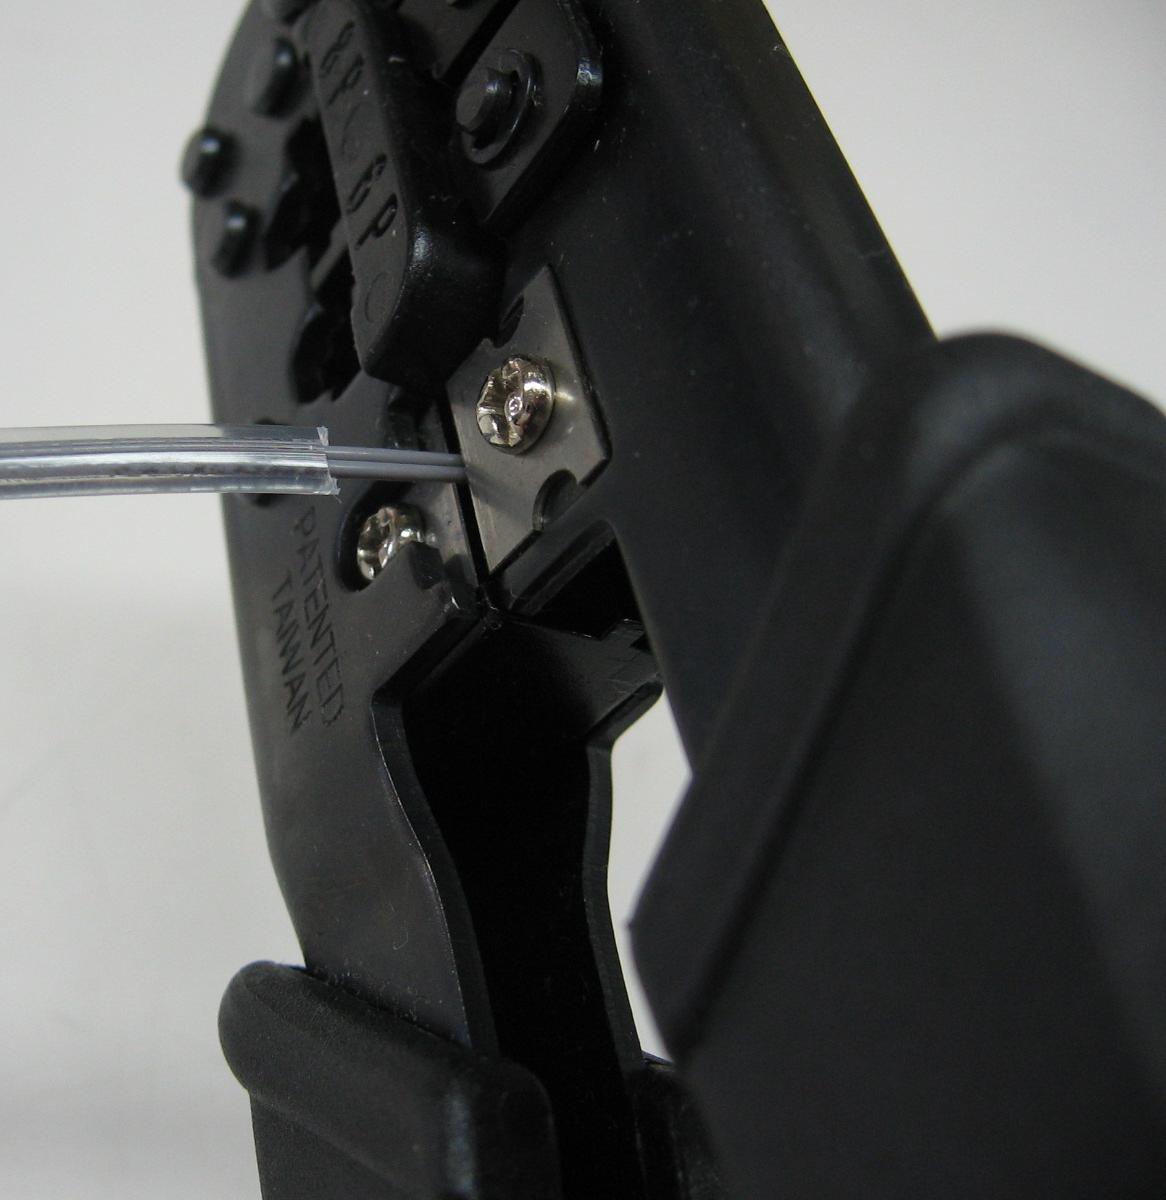
- Terminal-specific crimper: uses the die geometry and locator specified for that contact. A ratchet can enforce a full tool cycle, but it cannot make a mismatched die correct.
- Inspection tools: good light and magnification; production work may also require a crimp-height micrometer and calibrated pull tester.
Do not use pliers, side cutters, or an unrelated color-coded nest as a substitute for the specified crimp tool.
Strip without damaging the conductor
- Disconnect and verify power is off.
- Cut back to clean, undamaged wire.
- Set the strip length from the terminal specification—not a universal 3mm or 6mm rule.
- Strip straight off without cutting strands, scraping plating, or stretching insulation.
- Inspect every strand. If any are nicked, missing, folded back, or severed, cut off the end and start again.
Do not tin stranded wire before crimping unless the terminal manufacturer explicitly permits it. Added solder changes the conductor dimensions and flexibility and can prevent the specified compression.
Closed-barrel insulated terminals
- Verify the terminal’s wire range and the matching die.
- Insert the stripped conductor to the documented stop or inspection position. Insulation should not enter the conductor-crimp area, and bare strands should not extend where they can short to another contact.
- Place the terminal in the die exactly as the tool instructions show. Seam orientation is tool- and terminal-specific; do not rely on a universal “seam toward the anvil” rule.
- Cycle the tool fully without changing the wire position.
- Inspect the conductor location, insulation support, deformation, cracks, and exposed strands.
Open-barrel contacts
Open-barrel contacts commonly have separate wings: inner wings for the conductor and outer wings for insulation support. Correct results depend on the matching terminal, wire range, crimp height, strip length, and applicator.
A good inspection typically looks for a conductor brush visible past the conductor crimp, no strands in the mating or contact area, a suitable bellmouth where specified, and insulation positioned within its support wings. The exact limits come from the contact’s drawing or application specification.
Generic 0.1-inch hobby housings are often casually called “Dupont” connectors, but compatible-looking contacts can require different tools and dimensions. Identify the actual contact family instead of assuming every housing uses the same crimp.
How to check a crimp
- Visual inspection: confirms strand placement, insulation support, bellmouth, conductor brush, cracks, and terminal damage.
- Crimp height: for specified open-barrel systems, this is a key non-destructive process check and must be measured at the documented location with the correct instrument.
- Pull testing: use the terminal manufacturer’s test method and minimum force. A casual “pull hard” test is subjective and can damage a good termination.
- Electrical testing: may be required for production or safety-critical work, but continuity alone cannot prove that a crimp has acceptable resistance or mechanical strength.
A light handling check can reveal an obviously loose wire in a hobby project, but it is not a substitute for specified pull testing. If a crimp is outside specification, cut it off and remake it with a new terminal unless the manufacturer provides an approved rework procedure.
Common failure modes
- wrong wire, terminal, or die combination;
- strip length too short or too long;
- cut or folded strands;
- insulation caught in the conductor crimp;
- bare conductor extending into the mating area;
- insulation support crushed too tightly or left open;
- partial tool cycle, worn tooling, or incorrect locator position;
- solder added to a crimp system that was designed for bare conductor.
Crimp or solder?
Use the termination method specified for the component and environment. Board pads are commonly soldered; removable contacts and wire harnesses are commonly crimped. A correctly engineered crimp can provide low resistance and strong mechanical performance, but soldering and crimping are processes—not interchangeable upgrades. Do not add solder to a completed crimp unless its manufacturer explicitly requires or permits it.
Technical references
- Molex Industrial Crimp Quality Handbook — strip quality, conductor brush, bellmouth, crimp height, and pull-force factors.
- TE Connectivity: The Simple Guide to Crimping — matching strip length, wire placement, terminal, and tooling.
- TE Connectivity crimp-quality guidelines — visual checks and examples of conductor and insulation failures.
Choosing the right crimp connector for the job
Not all crimp terminals are interchangeable. Match the connector to the environment, not just the wire gauge:
- Insulated (vinyl) terminals — the familiar red/blue/yellow ring, spade, and butt connectors. Fine for dry, indoor, low-vibration hobby work: breadboard power rails, enclosure wiring, bench projects. Cheap and everywhere. Not for damp or outdoor use — the vinyl sleeve doesn’t seal.
- Heat-shrink terminals — have an adhesive-lined sleeve that melts and seals around the wire when heated. The right choice for automotive, marine, outdoor, or anywhere moisture exists. They cost 3–4× more per terminal, and they’re worth every cent in a car door or garden project.
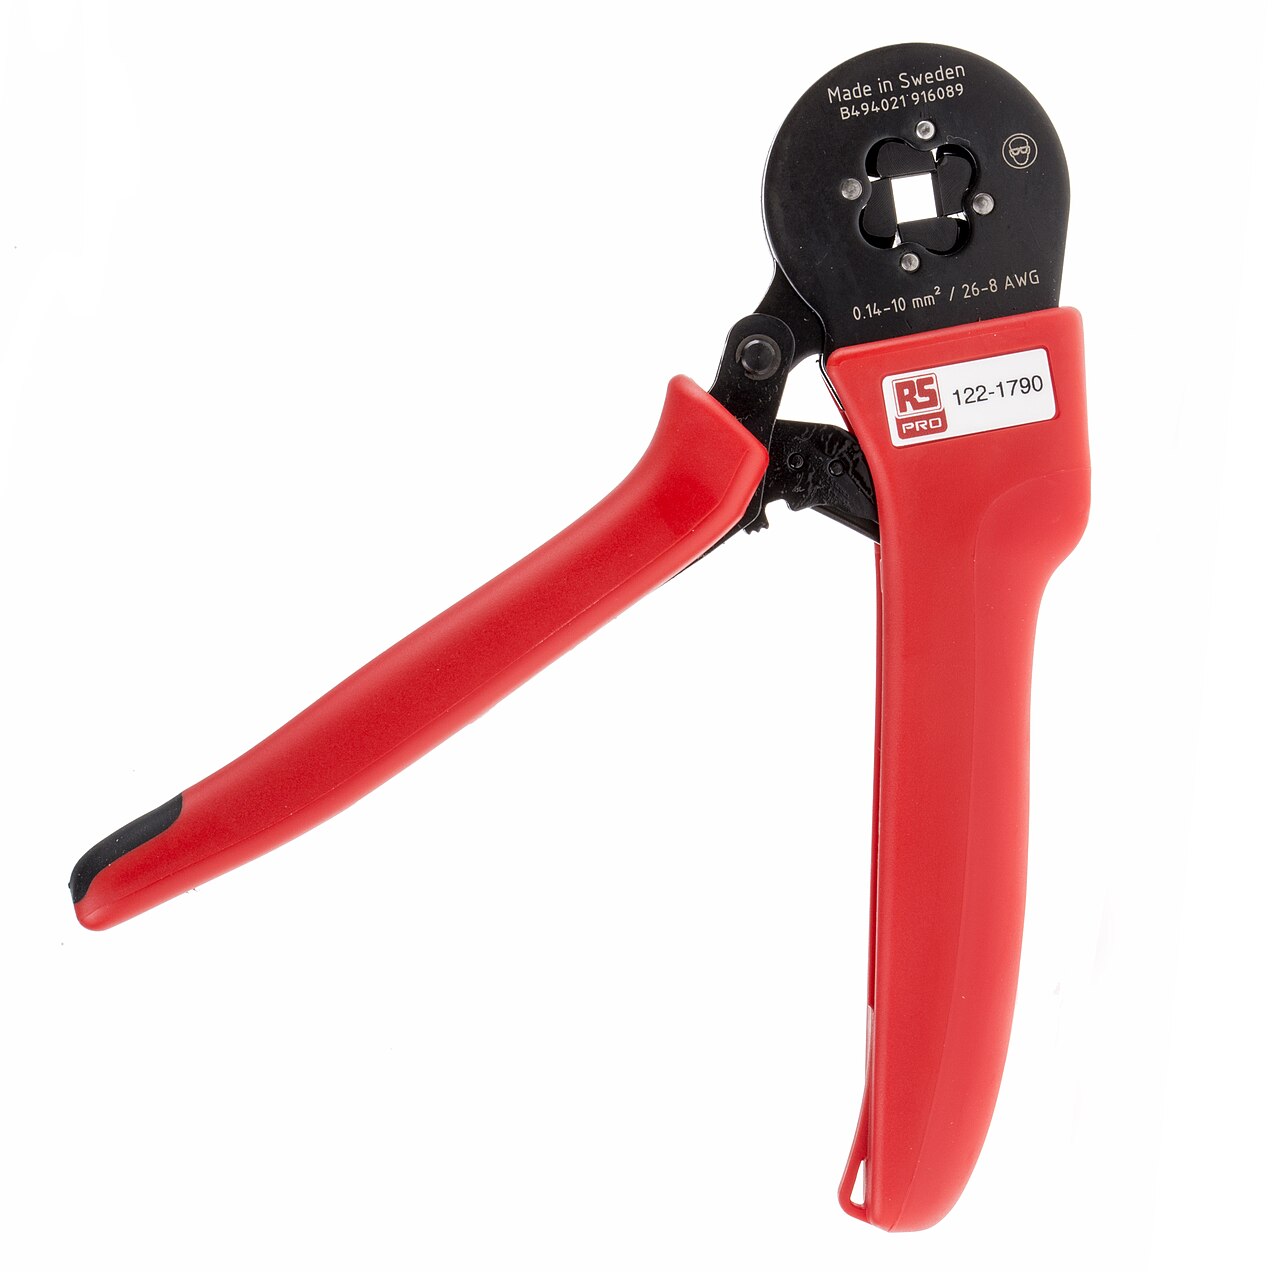
- Ferrules — tiny copper sleeves crimped onto stranded wire ends before they go into screw terminals or terminal blocks. They stop strands from splaying, breaking, or shorting to neighbors. If your project uses DIN-rail terminal blocks, barrier strips, or Euro-style connectors, ferrules aren’t optional — they’re the correct termination. Use a square-profile ferrule crimper, not pliers.
The honest rule: indoor bench project → insulated is fine. Anything that sees water, vibration, or temperature swings → heat-shrink. Screw terminals → ferrules, always.
The pull test: how strong is “strong enough”?
Every terminal manufacturer publishes a minimum pull force for each wire/terminal combination — typically in the tens of Newtons for small hobby terminals (for example, a common 22–18 AWG insulated terminal might spec 40–90N depending on the series). Look it up in the terminal’s application specification; that’s the real standard.
For hobby work without a calibrated tester, here’s a practical stand-in: grip the wire (not the terminal) and pull with firm, steady pressure — roughly what it takes to open a stiff jar. A good crimp won’t budge, slip, or elongate. If the wire slides out, stretches at the crimp, or the terminal deforms, cut it off and remake it. What you’re checking is that the strands and terminal have become one mechanical unit, not two parts friction-fighting each other.
Never “test” a crimp with a sharp yank. A violent jerk can damage a perfectly good termination and tells you nothing a steady pull doesn’t.
When to solder instead of crimp
Crimping isn’t universally better — it’s better where it’s specified. Solder when:
- You’re joining to a PCB pad. Pads are designed for solder. Don’t crimp to a board.
- The joint is tiny or delicate. Fine-pitch SMD work, small sensor leads, and repairs under magnification go better with an iron.
- It’s permanent and vibration-free. Inside an enclosure that never moves, a good solder joint lasts decades.
Crimp when:
- There’s vibration. Cars, drones, robots, appliances — crimps flex without cracking; solder wicks up strands and creates a stress point where the solder stops.
- It’s a harness or removable connection. Anything you’ll unplug, service, or reconfigure.
- You’re in the field. A crimper and terminals fit in a pocket; a soldering station doesn’t.
The real rule: match the method to the application and the manufacturer’s spec — not to whichever tool you happen to like more.
Crimp failures: what they look like
Learn to read a bad crimp by sight. Here’s the rogues’ gallery:
- The “wings” never closed: on open-barrel contacts, the conductor wings should curl inward and grip the strands. If they’re splayed outward or only half-folded, the die was wrong or the terminal sat crooked in the tool. The wire will pull out with modest force.
- Insulation trapped in the conductor crimp: you can see colored insulation pinched between the metal wings where only bare strands should be. This is the #1 beginner failure — strip length was too long. The crimp grips plastic instead of copper, and resistance climbs as it loosens.
- Cracked or split insulation sleeve: on pre-insulated terminals, a cracked vinyl sleeve means the die crushed too hard or the terminal was the wrong size. Moisture and shorts follow.
- The “birdcage”: strands splayed out around the terminal instead of inside it, usually from inserting the wire at an angle or with a frayed end. Trim, re-strip, and start over.
- Shiny, flattened, over-compressed barrel: the crimp looks pancaked rather than formed. Too much force work-hardens the copper and actually weakens the joint over time. Check your tool setting against the spec.
Related Reading
- How to Solder Electronics: A Beginner’s Guide to Clean, Strong Joints
- Electronics Basics: Resistors, Capacitors, and LEDs Explained Simply
- How to Use a Multimeter: The Beginner’s Guide to Testing Electronics
- Bench Power Supply for DIY Electronics: How to Choose, Set, and Use One
The DIY Geek — hands-on guides for electronics, 3D printing, woodworking, and smart home.